

Valve and faucet parts combine three different machining priorities
A valve stem may be mostly concentric turning. A faucet connector can add internal threads, sealing faces and wrench flats. A valve body or handle component may require radial holes, off-center drilling or milled profiles. Visible sanitary hardware also introduces surfaces that must remain suitable for polishing, plating or another specified finishing process. Separating these priorities—functional turning, secondary features and appearance surfaces—prevents a generic “brass CNC lathe” search from hiding the operations that actually drive machine selection.
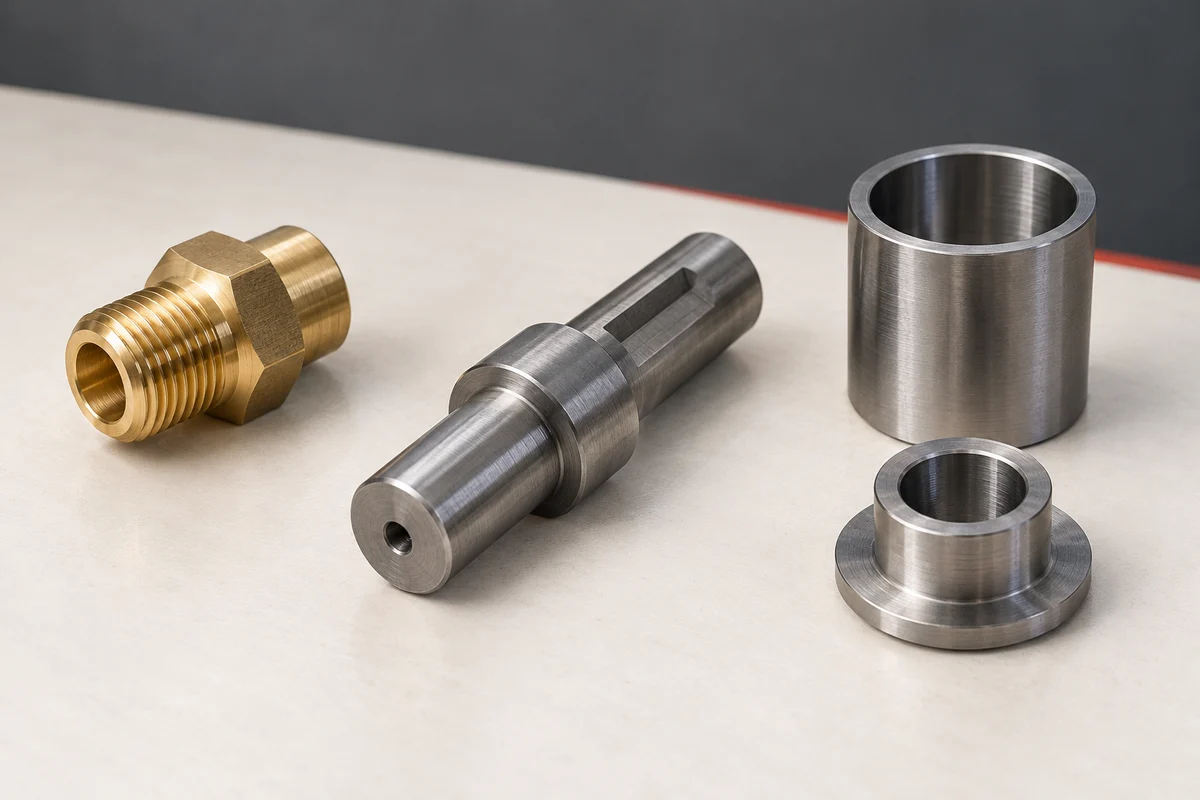
Use turn-mill machining when ports and profiles must stay aligned
The GDM-CX-Y55 is designed for single-setup turning, milling, drilling and tapping of chucking and disc-type parts. Its X/Y/Z axes and radial and axial live-tool heads support side holes, off-center holes and compound profiles, while its published application scope includes valve parts. For a faucet connector or valve component that combines a turned sealing diameter with a radial port, keeping these features within one setup may simplify the process route. The drawing must still confirm the maximum diameter, 45 mm bar capacity, tool reach and clamping method.

Choose between integrated hex-flat machining and a dedicated polygon machine
Wrench flats on valve fittings and faucet connectors can be treated in two ways. The GDM-HZ40-400 combines flat-bed turning with a fly-cutter power head for two-flat, square, hexagonal and octagonal profiles, plus drilling and tapping. It is suited to fittings, valve parts and components with wrench flats, with bar capacity up to 40 mm. The GDM-XF60 is a dedicated polygon milling machine for round workpieces, including valve parts, tool shanks and bolt or nut profiles, with a maximum machining diameter and length of 100 mm. Integrated machining suits parts where turning and flats belong to one route; dedicated polygon milling suits a production mix dominated by repeated flat or polygon features.
Simple sleeves and valve stems may not need a turn-mill center
If the part consists mainly of outside diameters, bores, grooves and threads, a gang-tool CNC lathe can be a more direct comparison. The GDM-T40-360 and GDM-46A arrange turning, drilling and tapping tools in a compact linear layout for small bar parts. This distinction matters when comparing a family of sanitary hardware: a threaded sleeve and a cross-drilled valve body may share material and batch size but not the same process. Avoid specifying live tooling simply because another part in the same product family needs it.
Small parts turn mill: check gripping space before combining operations
A short faucet connector can fit inside a nominal machine envelope yet leave too little exposed material for a side drill or milling cutter. Show the permitted gripping length, thin walls, protected sealing surfaces and the position of the final cut-off. For a family of valve stems and sleeves, identify which parts only need turning and which add cross holes or wrench flats. This helps compare a small-parts turn-mill route with a gang-tool route without adding driven tools to every part. Ask for an operation sequence showing when the part is turned, cross-drilled, deburred and inspected, and whether a second grip is required.
Plan machining around the finishing sequence
For brass or stainless valve and faucet parts, identify which surfaces control sealing or fit and which will remain visible after finishing. State the material grade, stock condition, polishing or plating sequence, protected dimensions, acceptable edge condition and surface-finish requirements. A machining route that is dimensionally correct can still create problems if a clamping mark appears on a visible surface or if later finishing changes a critical fit. These are process inputs, not cosmetic details to add after machine selection.
Build the inquiry around representative parts
Provide drawings for the smallest and largest parts in the family, plus one example with the most complex holes or flats. Include material, stock diameter, finished dimensions, thread and sealing standards, appearance-surface requirements, batch quantity and current secondary operations. This gives the machine discussion a real range to cover. The hydraulic-fitting guide is useful when sealing passages and side ports dominate; the threaded-parts guide is useful when the product family is driven by threads and hex profiles.