

A threaded part is rarely defined by the thread alone
A turned screw, stud or threaded sleeve may also include a shoulder, undercut, internal bore, sealing face, cross hole or hexagonal wrench section. Start with the bar diameter, finished length and thread standard, then mark every feature that interrupts the basic turned profile. A simple threaded sleeve can stay on a gang-tool CNC lathe; a connector with cross holes or wrench flats may justify a combined turning and milling process. This feature-based split is more useful than searching for one universal “fastener CNC machine.”
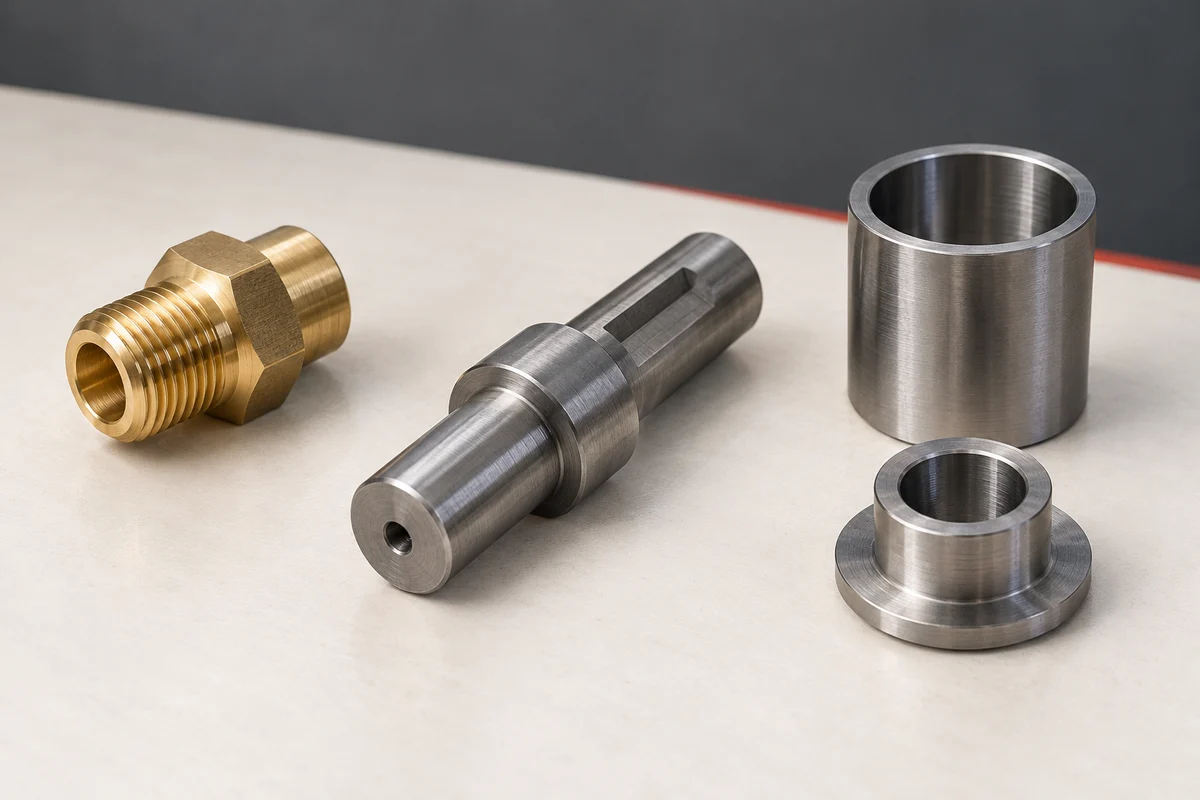
Gang-tool CNC lathes suit repeat bar-turned threaded parts
For bushings, pins, threaded sleeves and small connectors produced from bar, a gang-tool layout keeps turning, drilling and tapping tools in a direct linear arrangement. The GDM-T40-360 provides up to 40 mm bar capacity and 370 mm machining length, while the GDM-46A combines a 49 mm spindle bore, a 40 collet and machining lengths up to 400 mm. These published ranges make them useful comparison points for small and medium repeat parts, but the drawing still needs to confirm tool clearance, cut-off position and thread length.

Hex flats change the machine choice
Special nuts, hose fittings and threaded adapters often need two-flat, square or hexagonal profiles after the turned diameters and threads are complete. The GDM-HZ40-400 combines turning, drilling, tapping and powered fly-cutter polygon machining on one flat-bed machine; its published scope includes two-flat, square, hexagonal and octagonal features with bar capacity up to 40 mm. When polygon work is the dominant operation, the dedicated GDM-XF60 handles round workpieces up to 100 mm in machining diameter and length, with 40–50 mm bar capacity. The decision is therefore not simply “lathe versus mill,” but whether the part needs occasional flats within a turning cycle or repeated polygon machining as its main process.
Polygon turning machine or hex milling machine: what should you specify?
The names polygon turning machine, polygon turning lathe and hex milling machine do not fully define how the requested flats will be cut. Ask the supplier to explain the cutter motion, workpiece motion, tooling and supported profile for the proposed configuration. For GEDEMA, compare the dedicated GDM-XF60 polygon machine with the GDM-HZ40-400 turning and fly-cutter route described above. Specify across-flats size and tolerance, flat length, shoulders, corner requirements and material condition. A hexagon on the drawing is not enough to establish cutter clearance or the acceptable finished profile.
Fastener machining: separate hex-head cutting from the full production route
For screw-head polygon cutting or a special fastener machining lathe enquiry, state whether the blank is round bar, a preformed head or a partly machined part. Identify which operations remain: turning, thread cutting, polygon machining, deburring and inspection. If the specification also calls for heading, thread rolling, heat treatment or coating, list those as separate process requirements; a polygon-machine description does not establish a complete fastener production line. Compare any cycle estimate using the same material, tooling, loading method and inspection frequency. Include transfers and handling rather than assuming polygon cutting will always be faster than indexed milling.
Use the part family to compare cycle structure
A shop making one stud, one hex adapter and one threaded sleeve does not necessarily need the same machine for all three. Group the parts by bar diameter, overall length, external versus internal thread, number of tools, and whether radial features are present. A stable family of simple turned parts favors a straightforward gang-tool arrangement. Mixed threaded parts with flats, drilling or tapping benefit from evaluating a combined process. Dedicated polygon work can be separated when its volume and geometry justify it. This keeps the machine comparison tied to the actual product mix instead of a generic fastener label.
What to send for a threaded-part machine recommendation
Send the controlled drawing, material and stock form, annual or batch quantity, thread standard and tolerance, maximum bar diameter, required across-flats dimension, cross-hole details, cut-off allowance and inspection method. If several part numbers share one machine, include the smallest and largest examples. GEDEMA can then compare the drawing against the published product specifications rather than making a recommendation from thread size alone.