

A motor shaft should be described by its support and feature layout
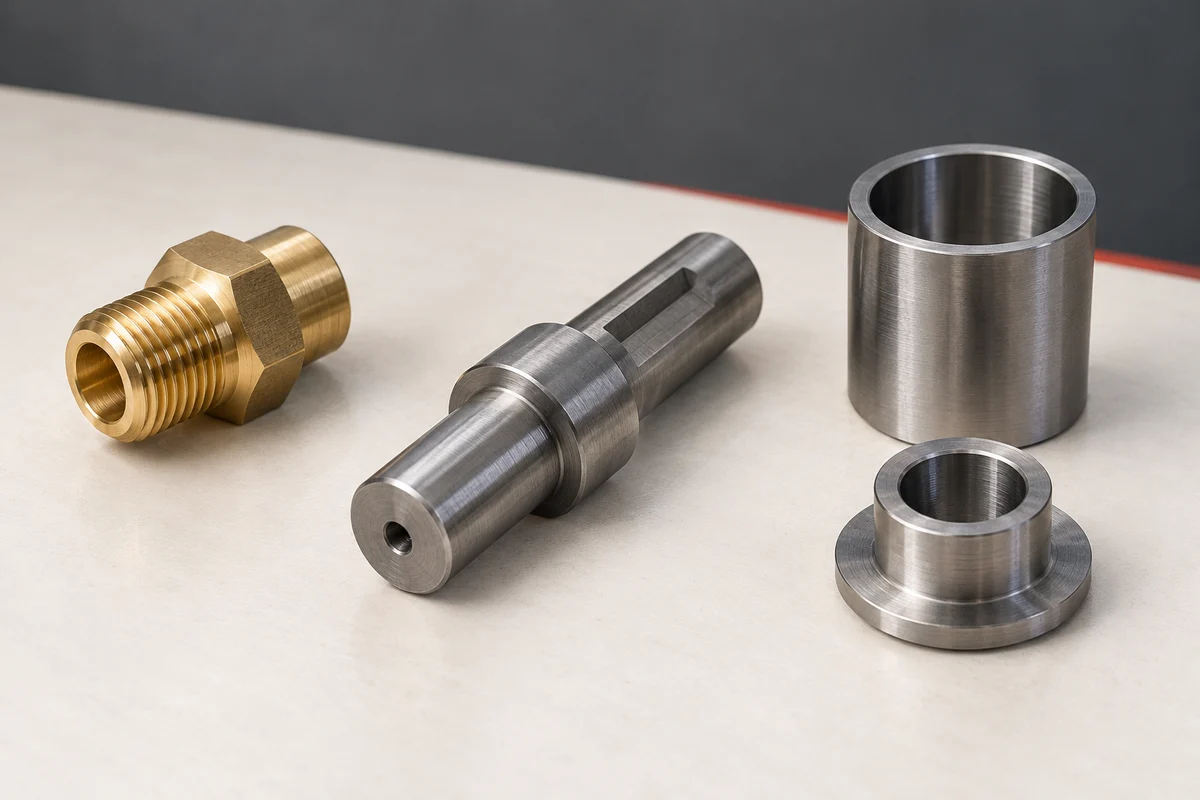
The shaft diameter alone does not define the machining route. Start with the finished length, stepped diameters, shoulders, bores, threads, keyway or flat requirements, and the positions that need support during turning. Also identify whether the drawing contains radial holes, milled flats or other features that interrupt a primarily turned profile. This separates a repeat turning discussion from a part that needs additional milling or drilling capability.
Slant bed vs flat bed CNC: compare the working layout, not just the angle
Slant bed and flat bed describe machine layouts; neither label alone establishes rigidity, part accuracy or a faster cycle. For the same drawing, compare the space for the chuck, tools and tailstock, operator access for setup, and the path for chips and coolant to leave the cutting area. Ask how the selected configuration handles the material and tool arrangement you intend to use. For compact sleeves and bar parts, GEDEMA publishes the flat-bed GDM-H40-360 and slant-bed GDM-T40-360. Longer-shaft work can start from the GDM-T80-650W below. Bed angle and casting details should be confirmed for the selected model rather than assumed from the category.
CNC turning center or metal lathe machine: define the production task
A metal lathe may use manual controls or CNC; the machine name alone does not specify the production configuration. When requesting a CNC turning center for repeat shafts, state the required tool arrangement, part family, support, material and batch size. A turret does not by itself mean live milling is available. A tailstock supports a workpiece and should not be confused with a second work spindle. Compare the machine and quote using the actual turning, drilling and milling operations, then confirm the selected controller, tooling and workholding in the proposal.
 Gang-tool and turret choices for compact repeat parts
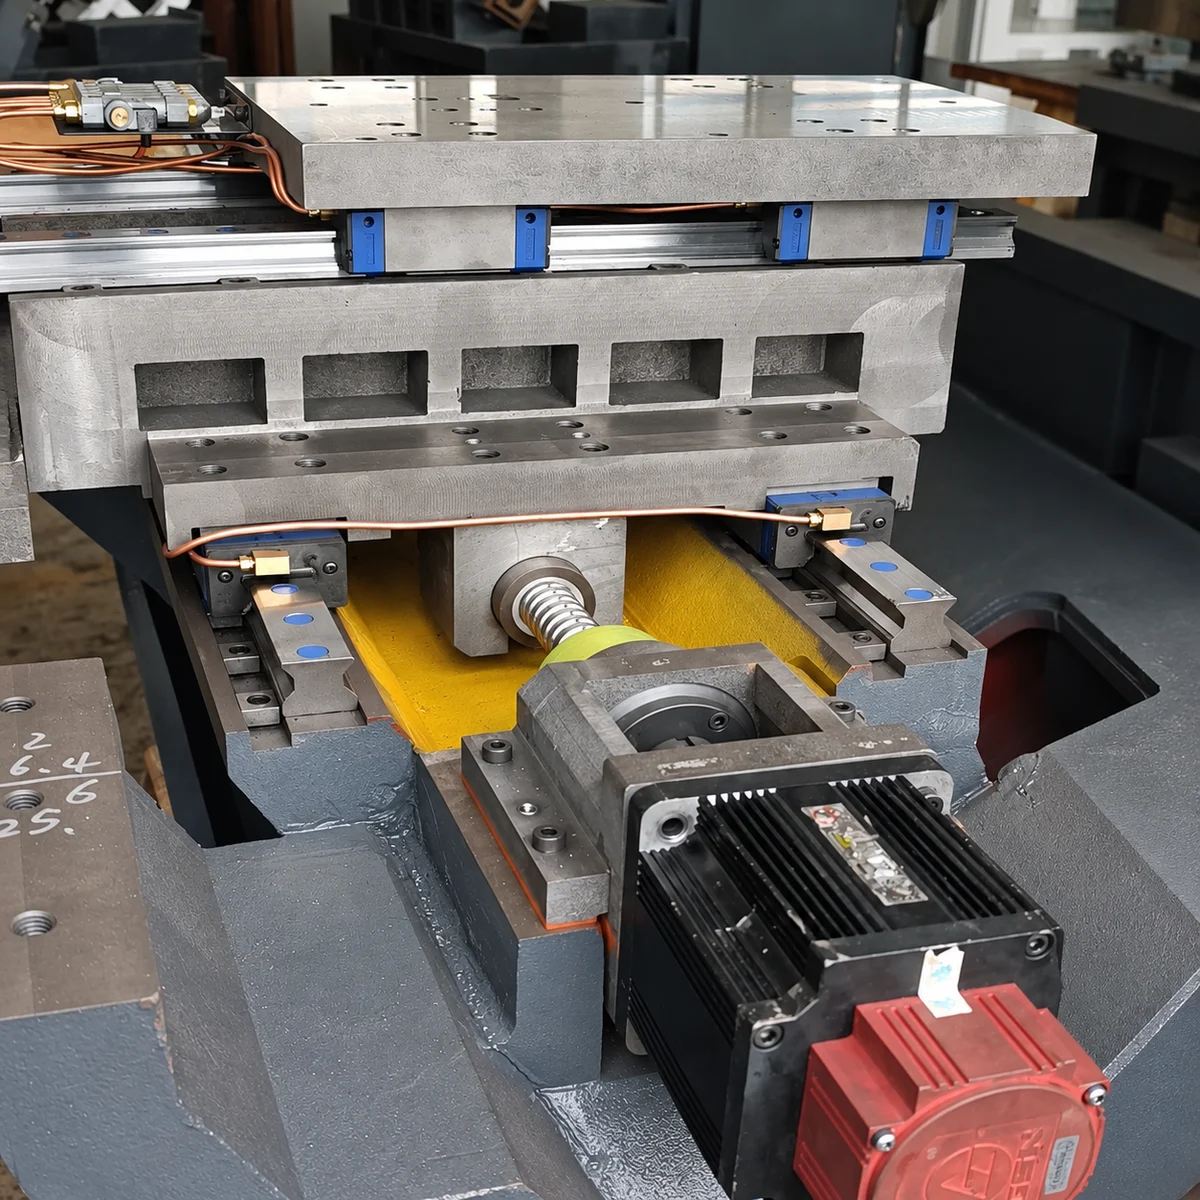
Use a longer-bed turning platform for repeat shaft work
The GDM-T80-650W is a slant-bed hydraulic servo turret CNC lathe for medium-size and longer shaft components. Its published capacity includes a maximum machining diameter of 400 mm, machining length of 630 mm and bar capacity from 48 to 65 mm. An 8- to 12-station hydraulic servo turret, 80 mm spindle bore and MT4 tailstock give a concrete starting point for reviewing shaft, sleeve, roller and coupling drawings. The drawing must still confirm the actual unsupported length, clamping method, tool access and inspection requirements.
Add turn-mill capability only when the shaft drawing needs secondary features
A shaft with drilled holes, milled flats or other secondary features may need more than turning. The GDM-CX80-650W is a CNC turn-mill center for medium-size shaft and bar components; its BMT40 live-tool turret supports turning, milling, drilling and tapping in one setup, and its tailstock helps support longer workpieces. Its published maximum machining diameter is 380 mm and machining length is 550 mm. Compare these ranges with the drawing rather than assuming that every motor shaft needs a turn-mill center.
Send the dimensions that control the process route
For a focused technical discussion, send the controlled drawing, material and stock form, smallest and largest diameters, finished length, support or tailstock requirements, end features, keyway or flat details, batch quantity and inspection method. If the part family includes both simple shafts and shafts with drilled or milled features, include representative examples of each. This allows the team to compare the drawing with published machine specifications without turning a general motor-shaft label into an unsupported machine recommendation.